Custom manufacturing
Formulations engineered around your market
From clinical dosing to flavour development, our R&D team builds products designed to win in your category.
Ingredient library
Audited raws, fully traceable
Every ingredient arrives with a certificate of analysis and is re-tested on intake.
- Spirulina & chlorella
- Organic matcha
- Grass-fed collagen peptides
- Whey & plant proteins
- MCT & acacia fibre
- Clinical probiotic strains
- Chelated minerals
- Adaptogenic botanicals
Flavour
Flavour & format development
- Natural berry
- Tropical mango
- Citrus mint
- Vanilla cream
- Unflavoured
- Chocolate cacao
Available as powders, capsules, gummies, sachets and ready-to-mix sticks.
Inside the factory
Where your product is made
A 12,000 m² certified facility covering blending, encapsulation, packaging, laboratory testing and export logistics under one roof.
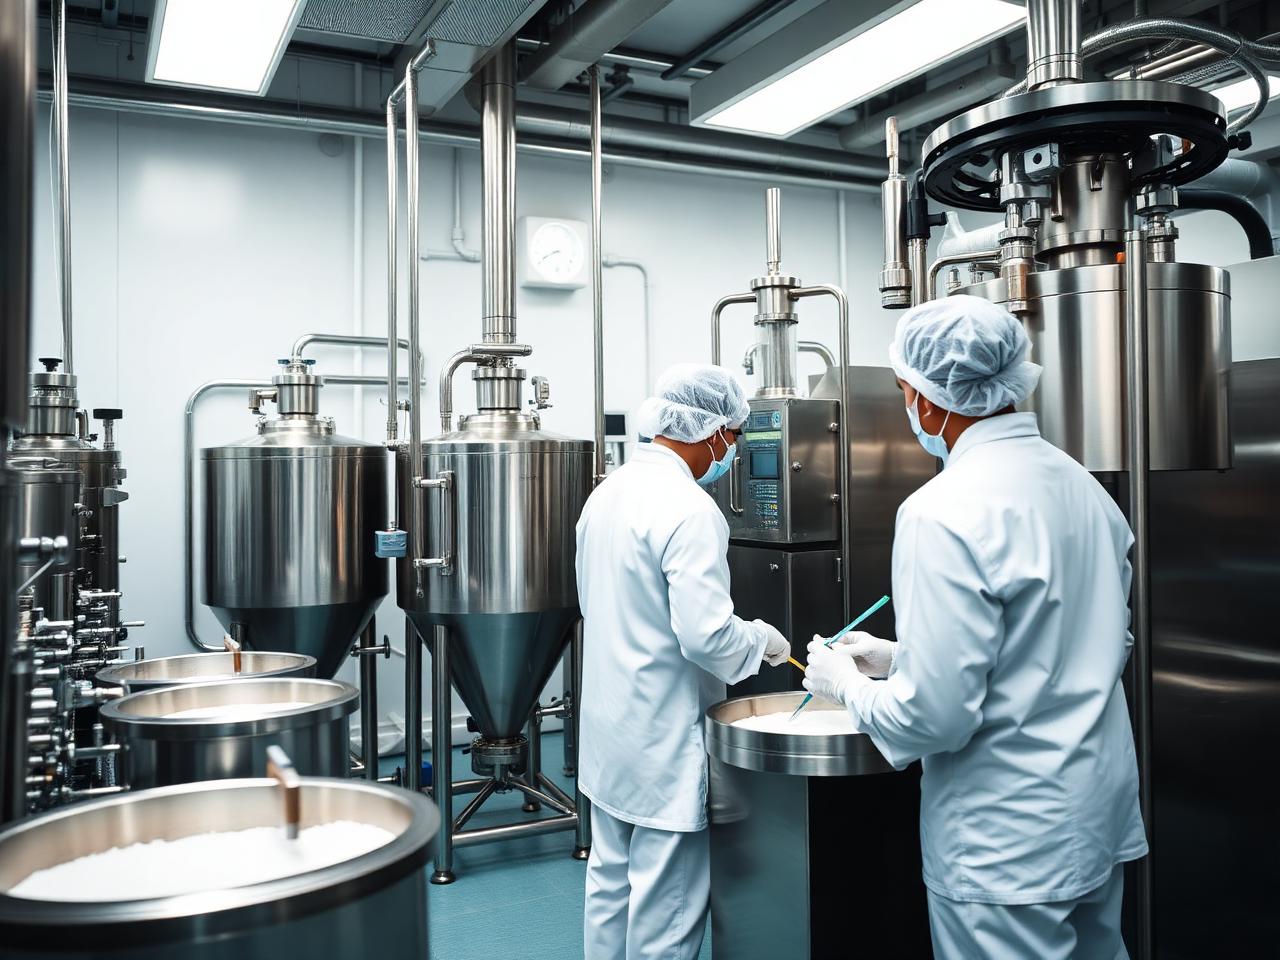
GMP blending suite
Climate-controlled cleanrooms with stainless-steel ribbon blenders for homogeneous, low-oxidation batches.
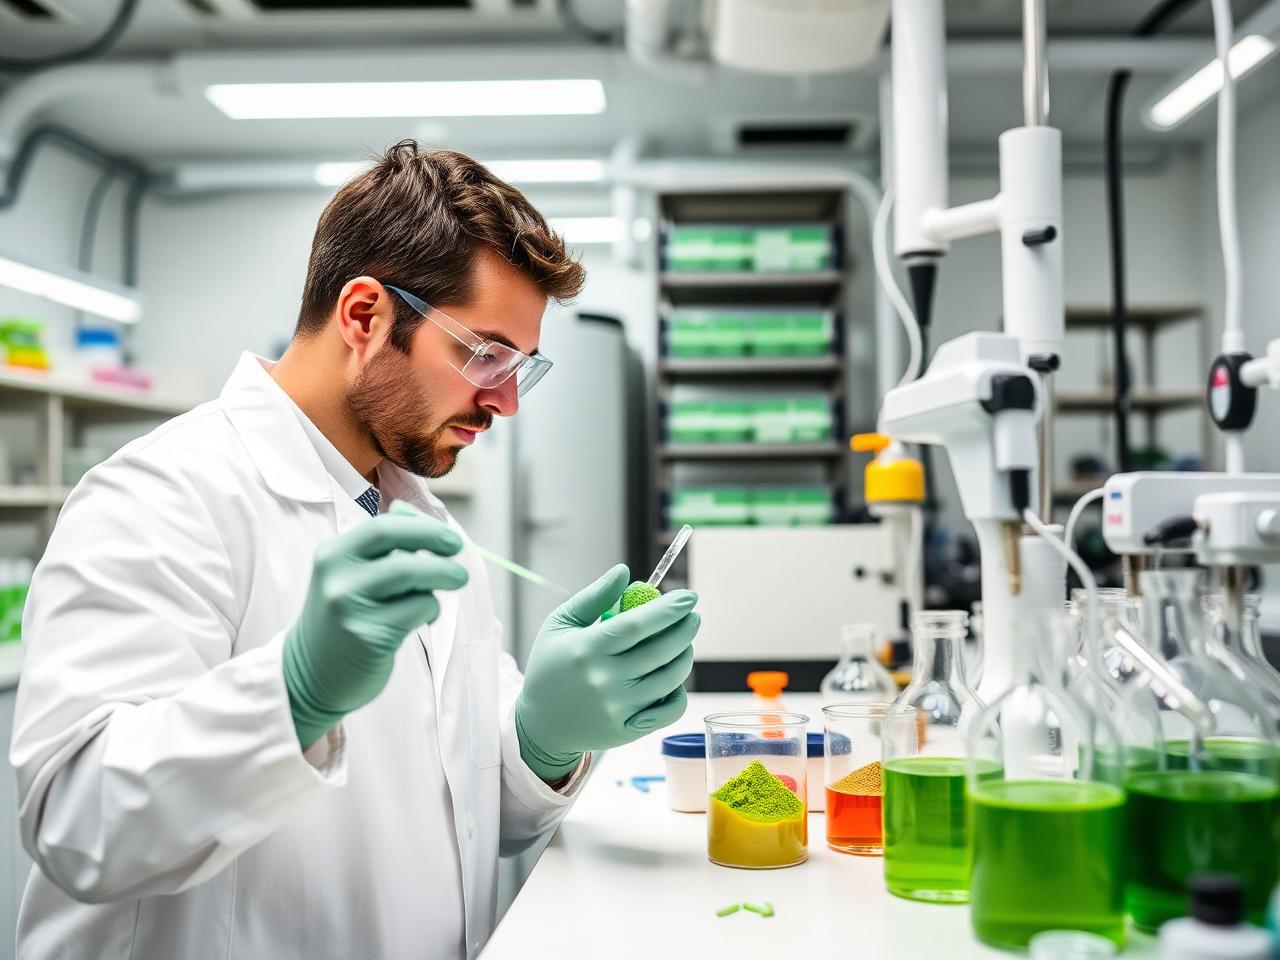
In-house QC laboratory
Heavy metals, microbial, potency and pesticide testing on every incoming raw and finished batch.
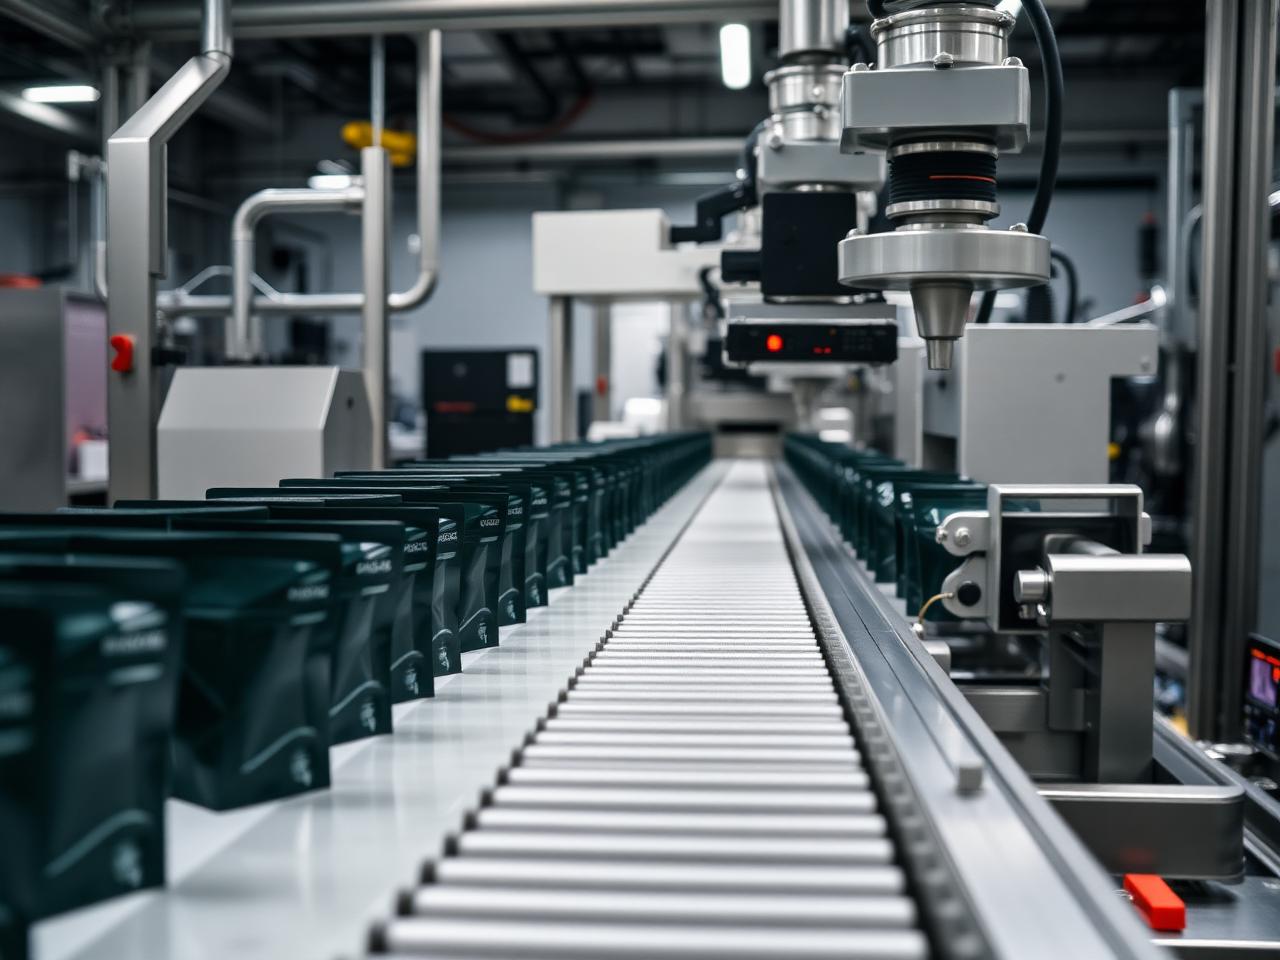
Automated packaging line
Nitrogen-flushed pouches, jars and sachets sealed, coded and weight-checked at up to 120 units per minute.
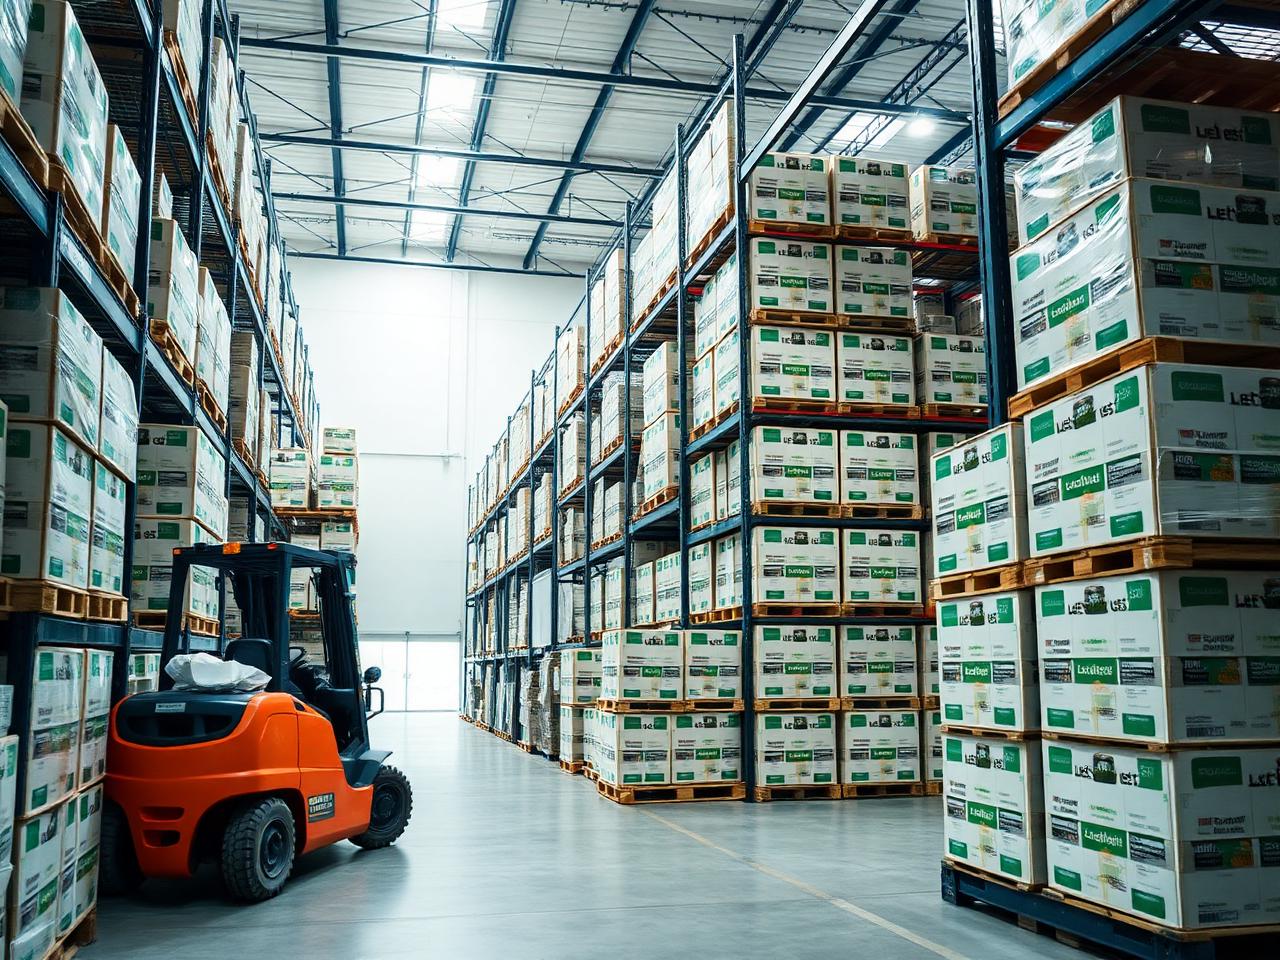
Temperature-mapped warehouse
Palletised, batch-traceable storage with export documentation prepared for 40+ destination markets.
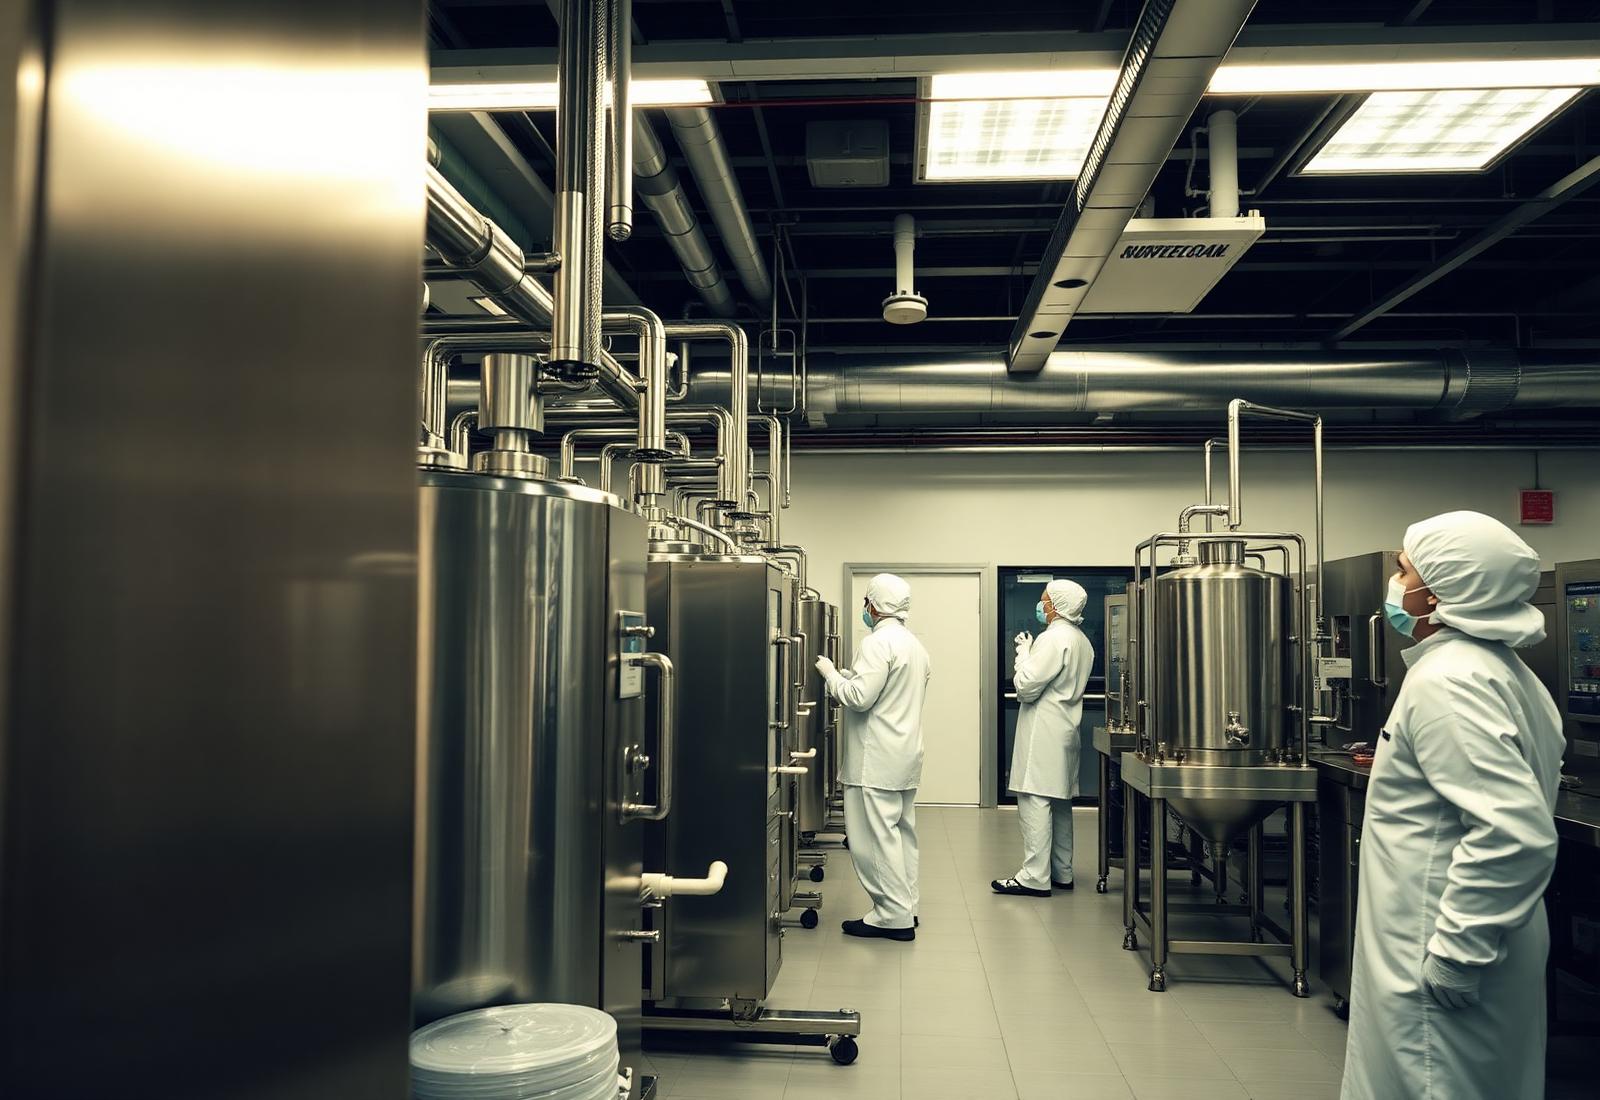
Production floor
ISO 22000 and HACCP certified facility running validated, fully documented manufacturing processes.
Certifications & quality
Trusted standards, independently verified
Our facility and processes are audited against global quality, safety and traceability standards so your brand is protected.
GMP certified
Manufactured in a facility that follows Good Manufacturing Practice guidelines for supplement production, hygiene and documentation.
ISO 22000 & ISO 9001
Certified food safety and quality management systems covering every step from raw material intake to finished goods release.
Third-party tested
Independent laboratories verify identity, potency, heavy metals, microbiology and contaminants so results are unbiased and defensible.
HACCP compliant
Hazard analysis and critical control points are monitored throughout production to prevent contamination before it happens.
Certificate of analysis
Every batch ships with a full COA covering raw material and finished product testing — ready for retailer and regulator review.
Export ready
Documentation prepared for EU, UK, US, GCC, ASEAN and Australasian markets including labels, certificates and stability data.
Product benefits
What makes a Leaf & Life formula sell
Every product we manufacture is engineered around efficacy, purity and repeat purchase — the three things that build a supplement brand.
Clinically relevant dosing
Actives are dosed at the levels used in published human trials — not fairy-dusted for a label claim, so your customers actually feel the difference.
Higher bioavailability
Chelated minerals, liposomal and micronised actives, and fat-soluble pairings such as D3 with K2 to maximise absorption per serving.
Clean-label formulas
No artificial colours, no added sugar, no unnecessary fillers. Natural flavour systems and stevia or monk-fruit sweetening as standard.
Purity you can prove
Every batch ships with a certificate of analysis covering identity, potency, heavy metals and microbiology — ready for retailer onboarding.
Shelf-stable to 24 months
Stability-tested formulas with moisture barrier packaging and nitrogen flushing, so stock survives long freight and warm climates.
Built for your market
Vegan, halal, kosher, gluten-free, keto and sport-tested variants with region-compliant claims, labels and language on request.
Timeline
A typical custom project
Week 1
Consultation
Week 2–3
Formulation & costing
Week 4–5
Sample production
Week 5–7
Stability & lab testing
Week 8–10
Full production run
Week 10–12
Freight & delivery